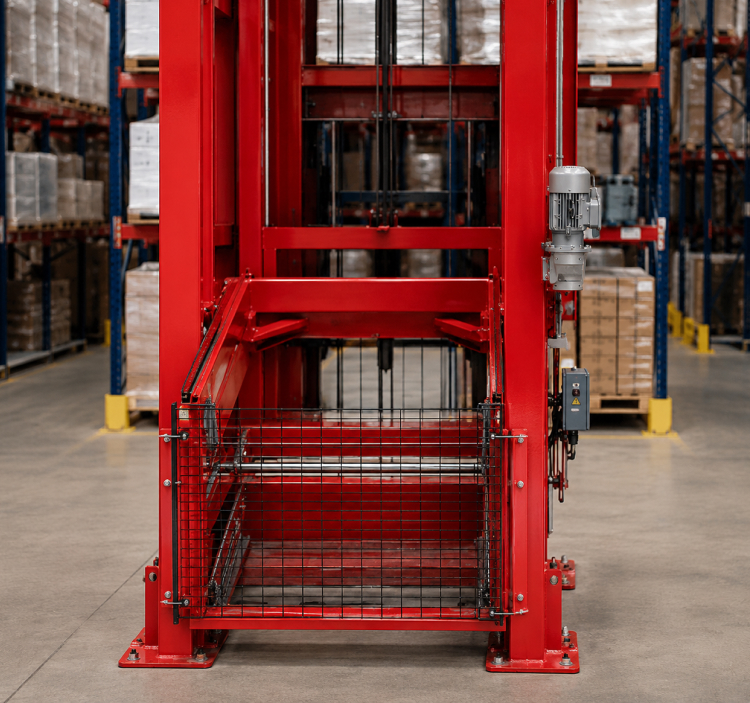
Vertical conveyor for light goods & pallet goods
Our conveyor units are built to suit each customer’s unique needs.
Vertical conveyors for efficient internal logistics
Vertical conveyors enable safe, efficient transport of goods between levels in warehouses, logistics facilities and production plants. They are particularly suitable where floor space is limited or where forklift traffic needs to be reduced.
The solution is adapted to the type of goods, the flow and the capacity requirements, and can be integrated with both new and existing conveying systems.
The load platform can be equipped with a roller or belt conveyor depending on the application. Frequency-controlled drive provides smooth movement and high precision, for a reliable and energy-efficient solution.

A spare parts package kept on site shortens lead times and reduces the risk of operational disruptions. It also means less time from your first call to a technician being on site. Contact us for advice!
5 reasons to invest in a new vertical conveyor
An effective way to optimise material flows between levels. By using the height of the building, you can increase capacity, free up valuable floor space and create a safe, flexible conveying solution for both light goods and pallet goods.

Safe, efficient transport between several levels
Less forklift traffic and improved internal logistics
Adaptable to different types of goods and flows
Can be integrated with existing systems
High reliability and low maintenance requirements
Free consultation
Get in touch and we will analyse your flow, calculate capacity and put together a proposal — free of charge.
Marketing Manager
Tommie Settergren




Frequently asked questions
To make things easier, we have gathered the answers to the most common questions in one place. Whether you want to know more about our services, deliveries or how to reach us, we hope you will find the answer here. Still can’t find what you are looking for?
What is a vertical conveyor?
A vertical conveyor is an automated conveying solution used to move goods between floors or levels. It can be adapted for both light goods, such as cartons and parcels, and heavier loads such as pallet goods.
How does a vertical conveyor work?
The vertical conveyor raises and lowers goods between stations and is often integrated into an existing conveyor system. The load carrier can be designed with a roller conveyor, chain conveyor or belt conveyor, for example, depending on the type of goods and the requirements.
What benefits does a vertical conveyor offer?
A vertical conveyor makes internal flows more efficient, reduces the need for manual transport and allows the available floor space to be used more effectively. It also improves safety and productivity.
Can vertical conveyors be adapted to our needs?
Yes — vertical conveyors can be tailored for different types of goods, lifting heights and transport requirements. They can be integrated into both new and existing conveyor systems and designed for through-transport or two-way traffic.